
Inconsistent yogurt texture or acidity can arise at several points in the same production line. Compare the batch records before changing the culture dose, processing settings or equipment.
Start with three checks: the starter system and dose, the batch temperature–pH record, and hygiene at product-contact points. Uncontrolled reuse of finished yogurt can introduce variability; commercial DVS cultures and a properly controlled bulk-starter process are different production methods. Compare these records before changing equipment or the recipe.

Compare a consistent batch with a defective one using the culture lot, dose, temperature–pH record and samples collected before and after cooling. Start with the first stage where the records or samples differ.
Is Your Starter Culture the Source of Inconsistency?
First identify what is actually being added to the vat: a concentrated direct-set culture, a bulk starter prepared under a controlled procedure, or yogurt retained from a previous production batch. They require different dosing and handling controls.
Commercial DVS/DVI cultures are concentrated starters used for direct inoculation or for preparing a bulk starter. A controlled bulk-starter process includes its own preparation, hygiene and activity checks. It should not be confused with repeatedly using finished yogurt without those controls.
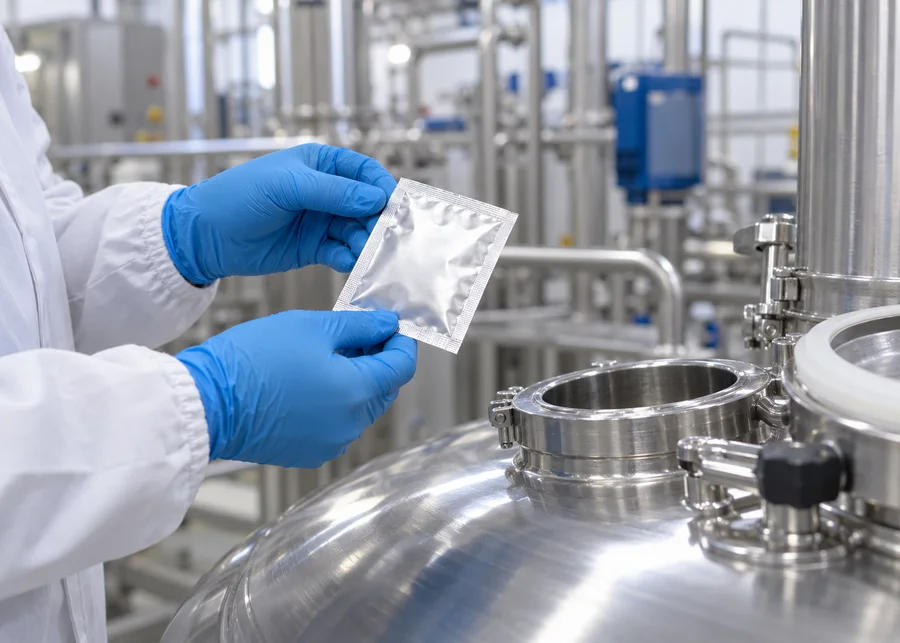
Before blaming the fermenter, compare a good batch and a poor batch. Check the culture product and lot, storage history, weighed dose, milk volume, inoculation temperature and time taken to reach the target pH. This shows whether the change starts with the starter or later in the line.
For DVS, use the culture supplier's units or mass for the stated milk volume. A percentage used for a liquid bulk starter cannot be transferred to a concentrated DVS product. For bulk starter, record the percentage basis, activity test, preparation time and holding conditions.
| Factor | Production Check | Error to Avoid |
|---|---|---|
| Culture System | Identify DVS/direct inoculation or controlled bulk starter | Treating every starter as interchangeable |
| Dose | Record culture units or mass and batch milk volume; for bulk starter, define the percentage basis | Using 2–4% as a universal DVS dose |
| Handling | Keep product-contact tools clean and sanitized; protect the culture during addition | Uncontrolled exposure or carry-over from previous batches |
| Milk and Fermentation | Check inhibitor test results and compare temperature–pH records | Changing the dose before checking the milk and process |
At NexAgri Solutions, we plan the Dairy Production Line around the chosen culture workflow. Specify the inoculation point, product-contact fittings, cleaning access and sanitation sequence together with the fermentation-tank requirements. Hygienic production depends on how these parts work together.
Are Your Processing Parameters Precisely Controlled?
Check actual product readings against the approved recipe at heating, homogenization, fermentation and cooling. Review sensor calibration and the sampling point before attributing a difference to the machine.
After checking the culture and milk, compare the heat-treatment record, homogenization conditions, fermentation pH curve and cooling profile. A change at one of these stages can affect texture, acidity or chilled shelf life.

Use the same measurement points and instruments when comparing batches. Record actual product conditions as well as controller set points, and note interruptions, delayed transfers or changes in filling time.
Compare these control points with the product specification:
- Homogenization and heat treatment: Record pressure, product temperature, flow and the heat-treatment time–temperature profile. Compare them with the validated yogurt recipe and the machine instructions. Homogenization changes fat dispersion; heat treatment also affects the protein network. Specify these duties together when selecting Plate Pasteurizers.
- Fermentation: Follow the culture and product specification for incubation temperature and target pH. Compare the time–pH curve across batches and investigate deviations. For Processing Equipment, specify temperature control, agitation and cooling requirements for the intended yogurt process.
- Cooling: Once the target pH is reached, follow the product’s cooling profile to slow culture activity. Track product temperature and pH during cooling and chilled storage, since some cultures continue to acidify after cooling.
Is Your Equipment and Environment Undermining Your Quality?
Inspect the product-contact route as well as the room. Valve seats, gaskets, poorly drained branches and exposed filling points can carry contamination into a batch even when visible surfaces look clean.
Your equipment and production environment must be impeccably clean. Inadequate Cleaning-In-Place (CIP) procedures leave behind residue and bacteria that spoil new batches, while a contaminated environment can introduce spoilage organisms at any stage, leading to defects like off-flavors or premature spoilage.

Compare cleaning records with the actual circuit and inspect difficult-to-clean fittings. Include hygiene results from the site’s verification plan when investigating off-flavors, gas production or early spoilage.
Key Areas for Hygiene Control:
- Cleaning-In-Place (CIP): Review the wash sequence and records for each circuit, including valves, branch lines and tank spray coverage. For NexAgri Cooling Tanks and Turnkey Projects, match cleaning access and CIP connections to the equipment layout and the site's verified cleaning procedure.
- Environmental Control: Check condensation, airflow around exposed product, personnel movement, drains and packaging-material handling. Set the cleaning and disinfection programme around those contamination routes rather than relying on one room-treatment method.
- Packaging: Match the Packaging Equipment to the yogurt's filling and chilled-distribution process. Check cleaning and sanitation of the filler, protection of cups and lids, seal integrity and the time before refrigeration. Specify an aseptic system separately when that is the actual process requirement.
Record the finding, corrective action and subsequent product checks for the affected stage. This helps the team distinguish a repeatable correction from an isolated good batch.
Conclusion
Use batch records to find where a good batch and a poor batch first diverge: culture addition, heating, fermentation, cooling or filling. Correct that stage, verify the result in finished-product checks, and keep the settings and cleaning records that made the improvement repeatable.

